Chemical Overhead Crane High-pressure Long-distance Positioning System Selection
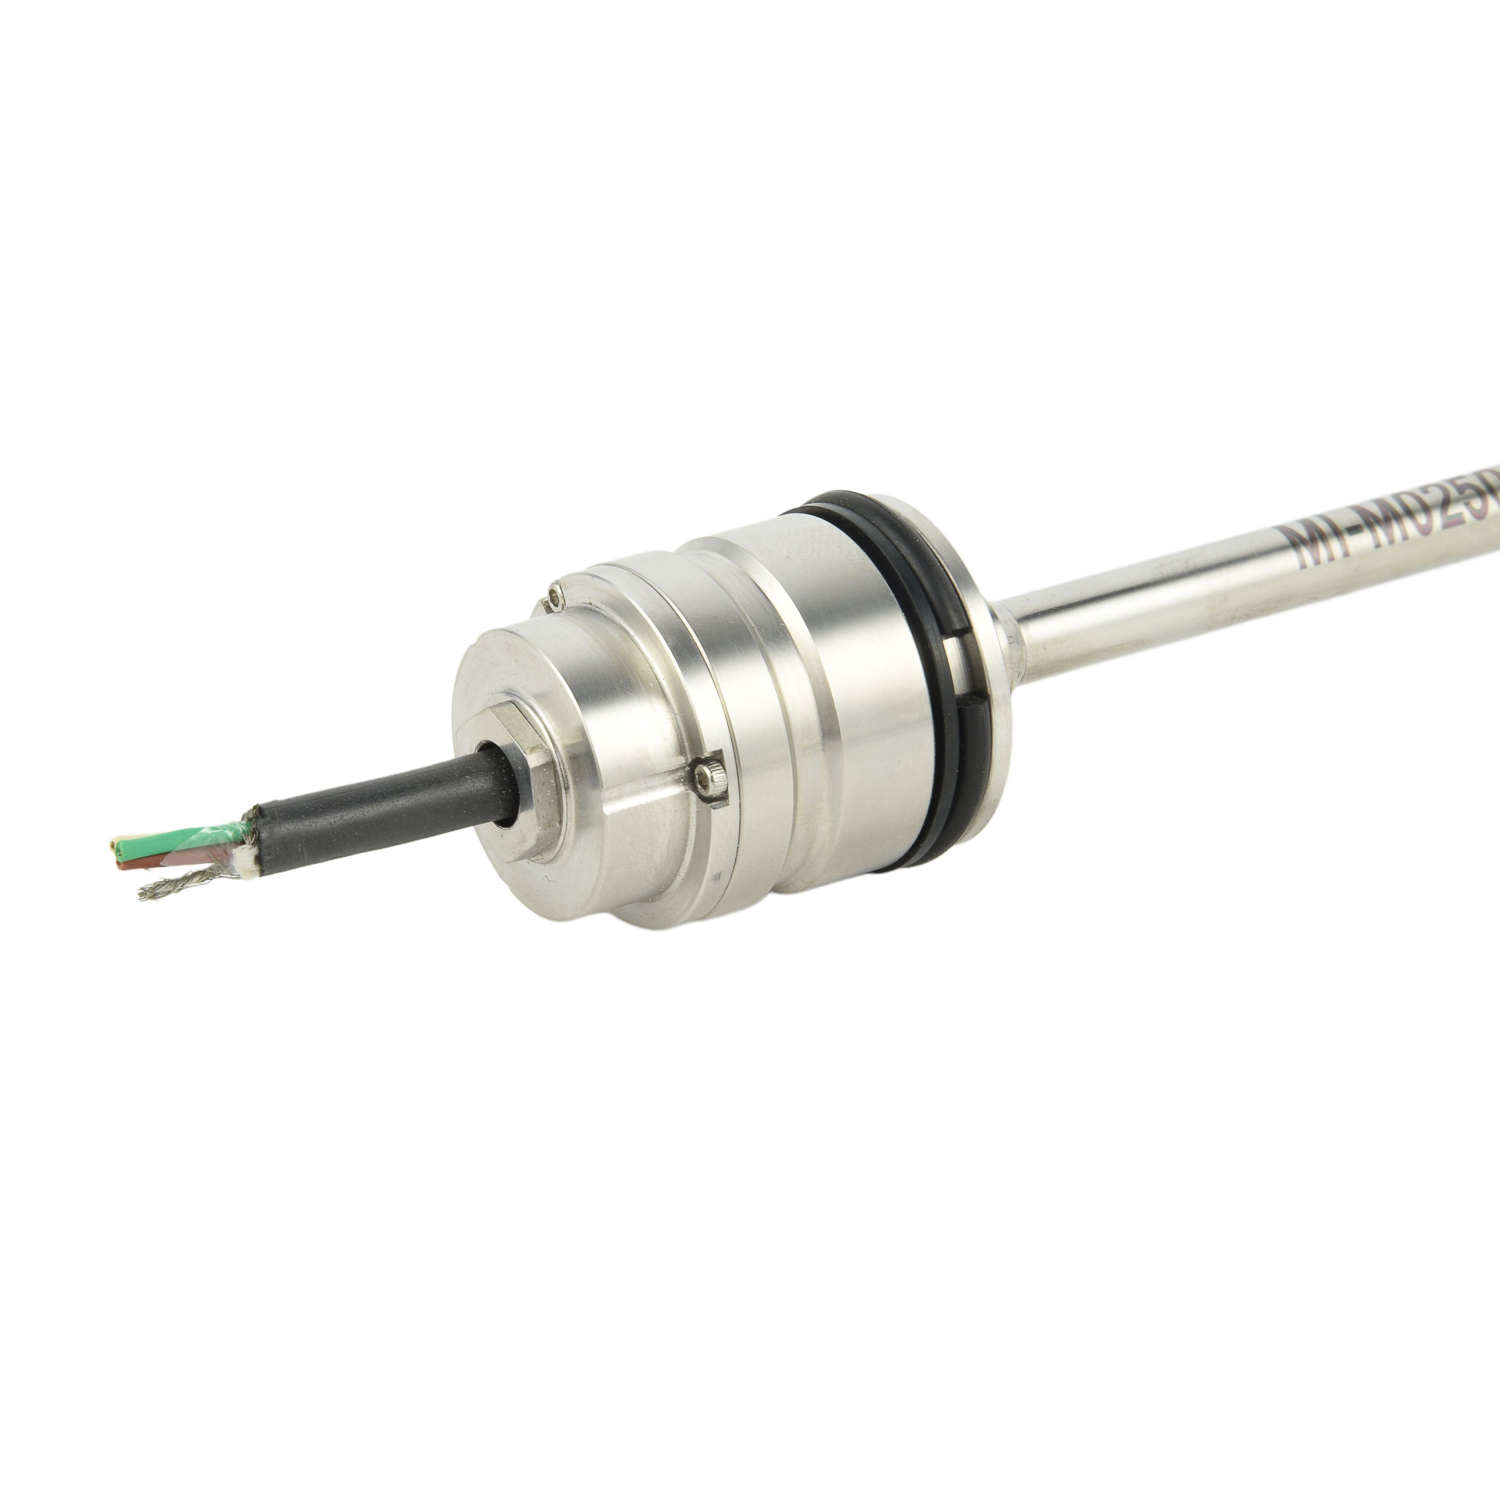
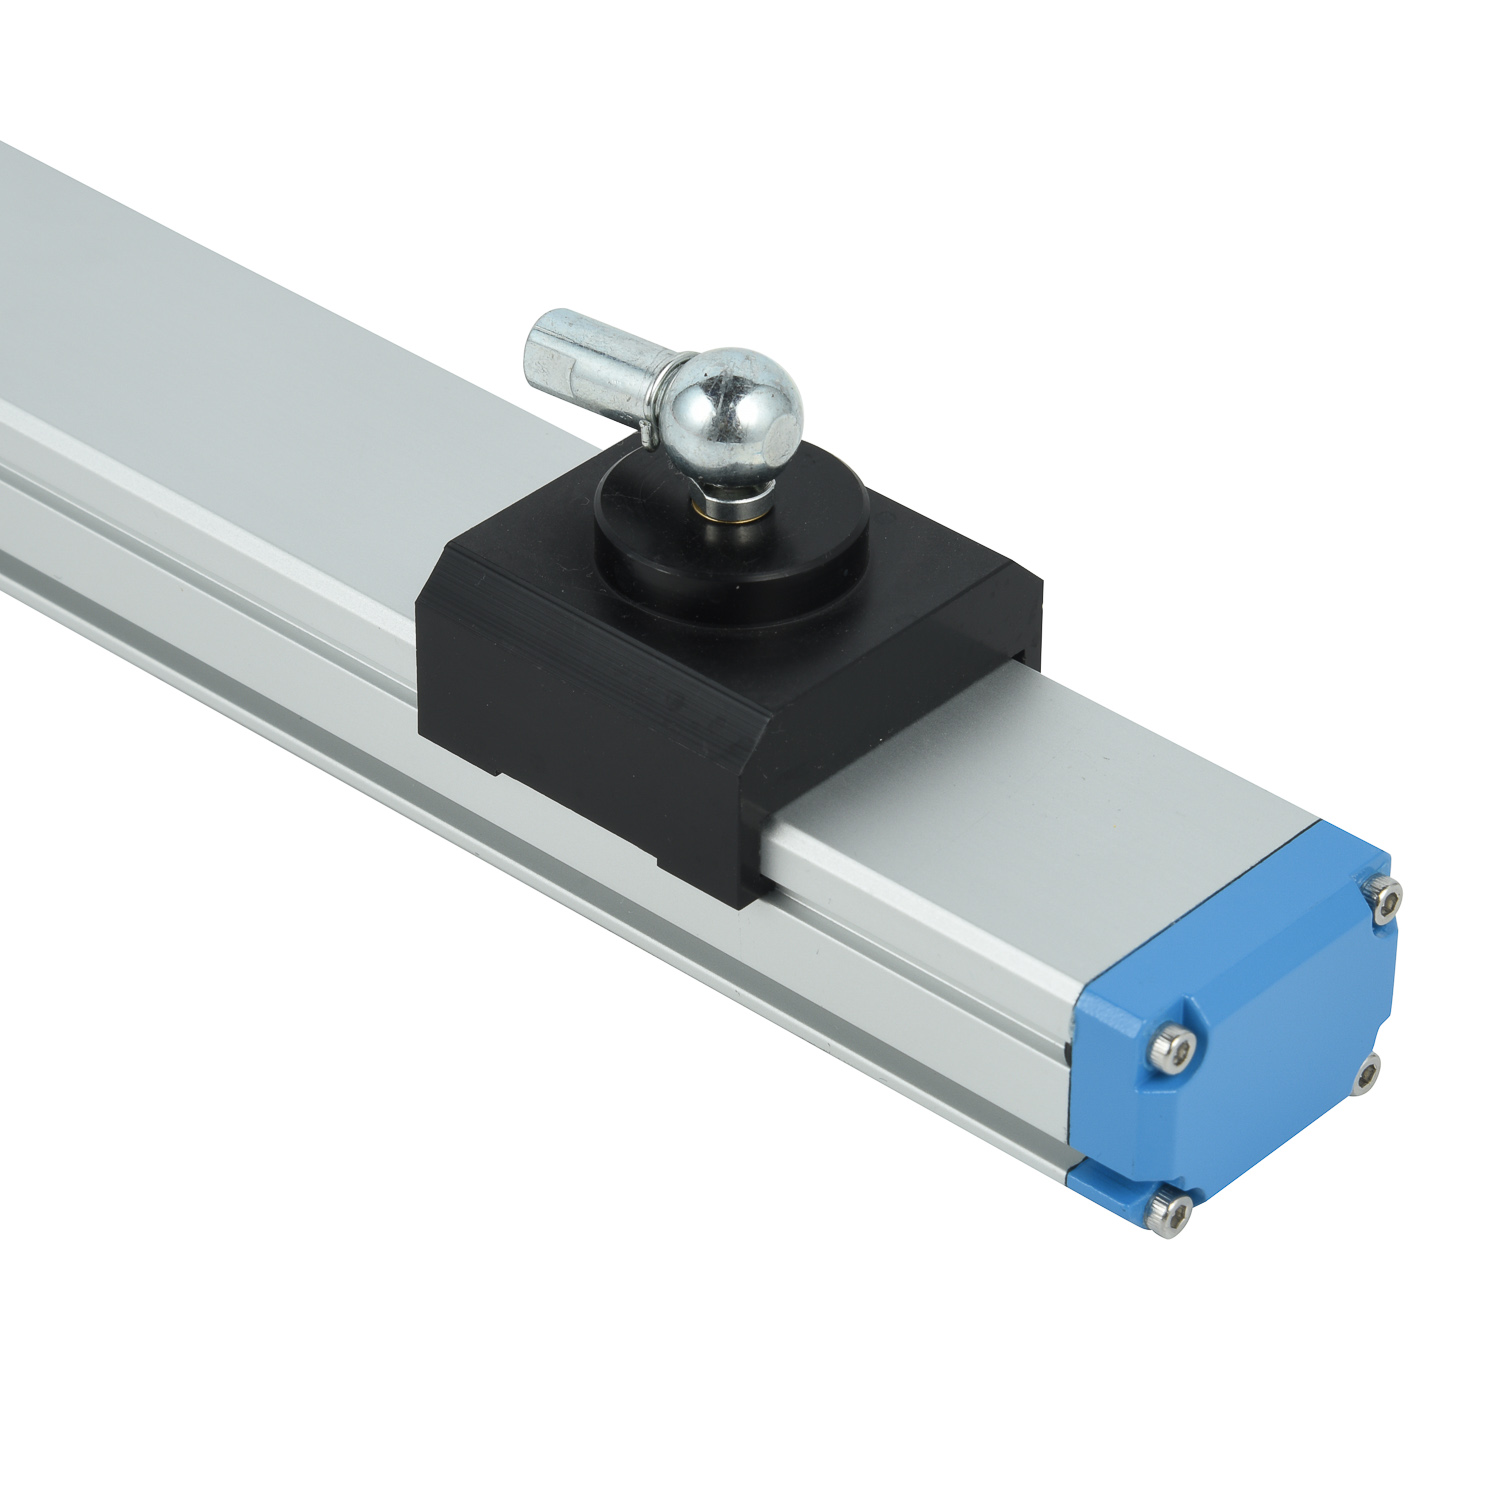
Selecting a positioning system for chemical overhead cranes requires a balanced review of safety, accuracy, and durability. The system must resist corrosive vapors, high-pressure washdown, dust, and vibration while maintaining reliable long-distance communication. First, confirm explosion-proof and ingress protection ratings for the crane area. Choose sensors and controllers certified for the classified zone, with stainless-steel or coated housings. Second, define required positioning accuracy and repeatability. For long travel and cross-travel movements, absolute encoders, laser distance sensors, or coded cable systems often outperform simple limit switches. Third, evaluate high-pressure cleaning. Look for sealed connectors, IP66/IP67 components, and protected cable routing that can tolerate washdown without signal drift. Fourth, test long-distance performance. Signal latency, cable voltage drop, and electromagnetic interference from motors and chemical equipment can reduce precision. Prefer robust industrial protocols, shielded cabling, and redundant feedback. Fifth, integrate the system with crane PLC, anti-sway control, and safety interlocks. A clear HMI and diagnostic alarms shorten maintenance. Finally, compare lifecycle cost, spare parts, calibration effort, and supplier service. A suitable system should deliver stable positioning, safe operation, and low downtime under harsh chemical conditions. Document calibration records and spare-parts availability to support long-term reliability.
 Bridge Crane Corrosion-resista
 Crane Waterproof Crane and Tro
 Overhead Crane High-pressure C
 Stacker-reclaimer High-tempera