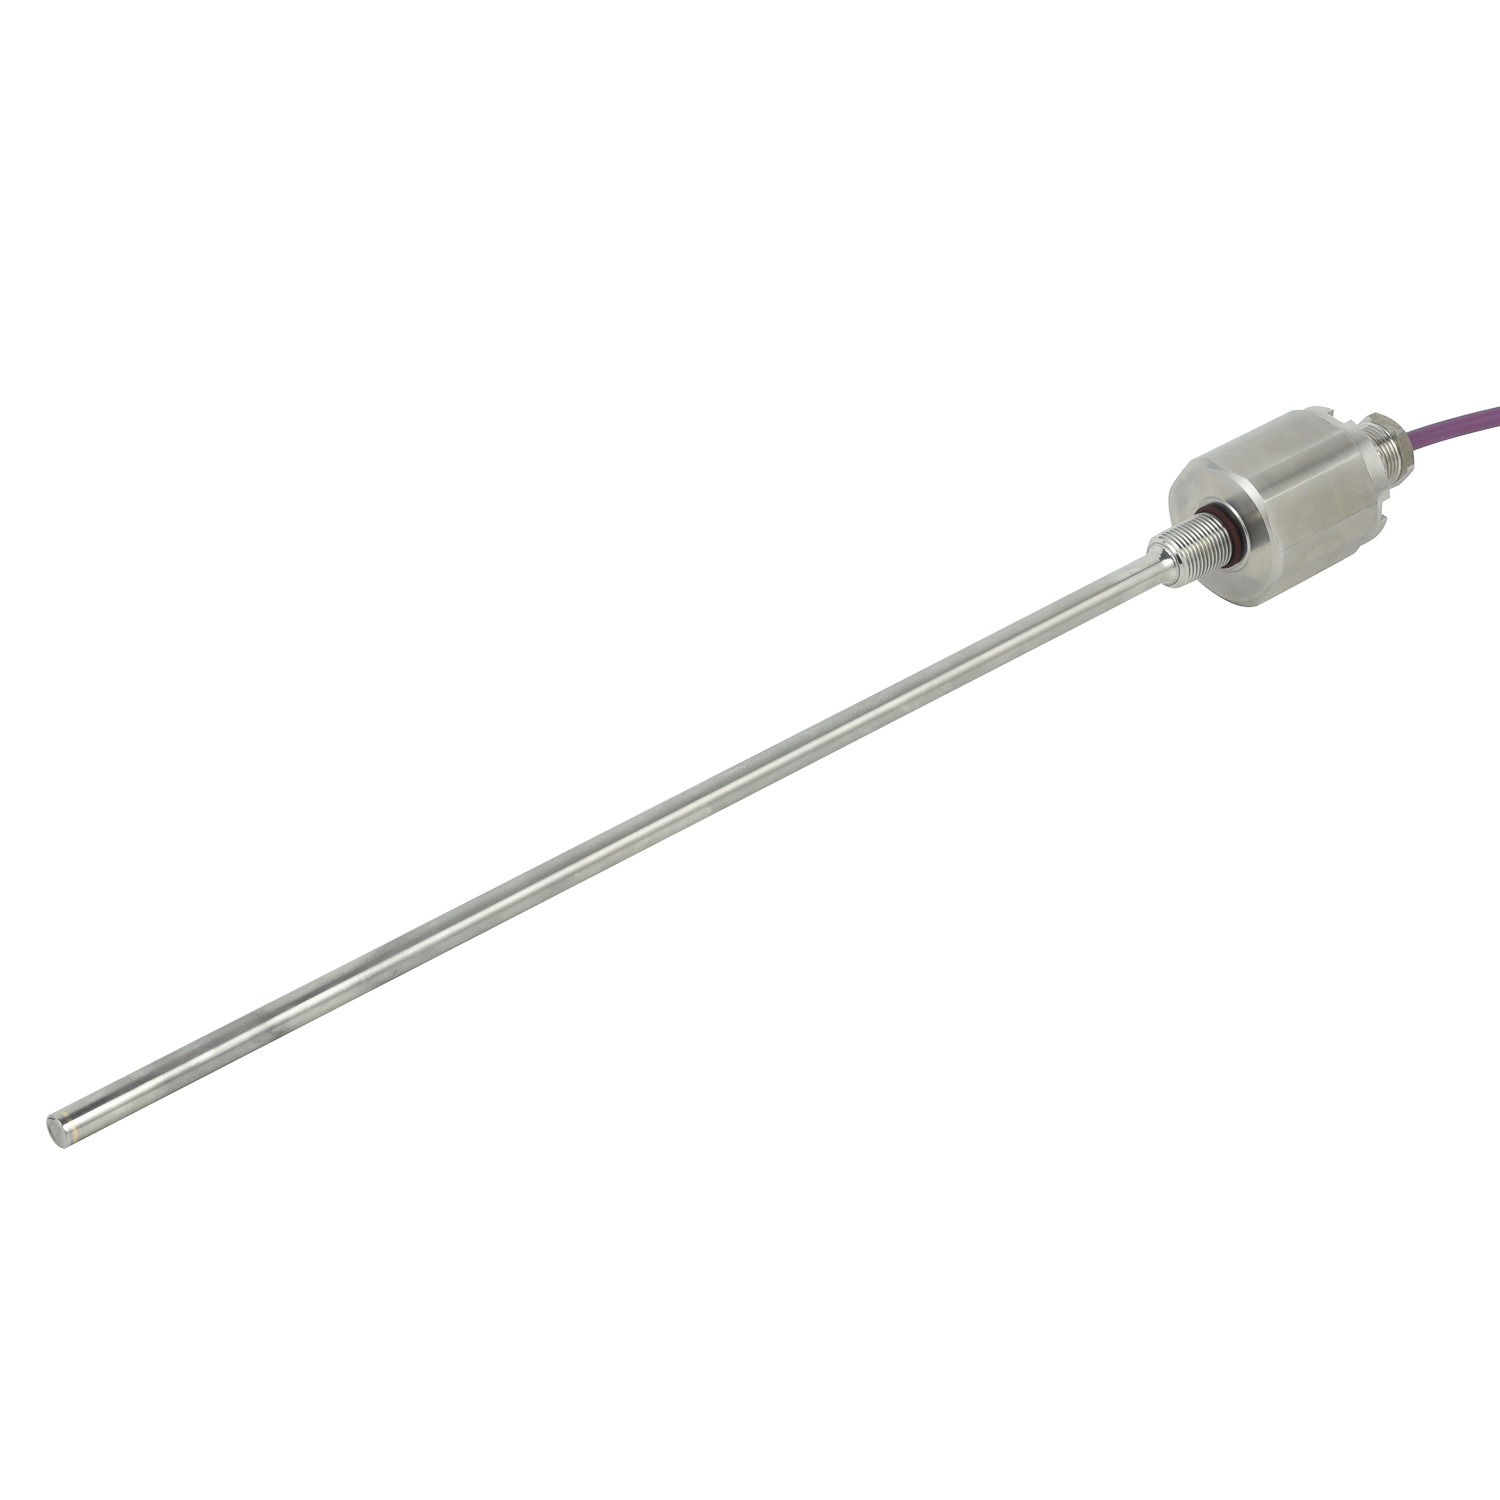
Cement Bucket Wheel Stacker-reclaimer Explosion-proof Magnetostrictive Displacement Sensor Price
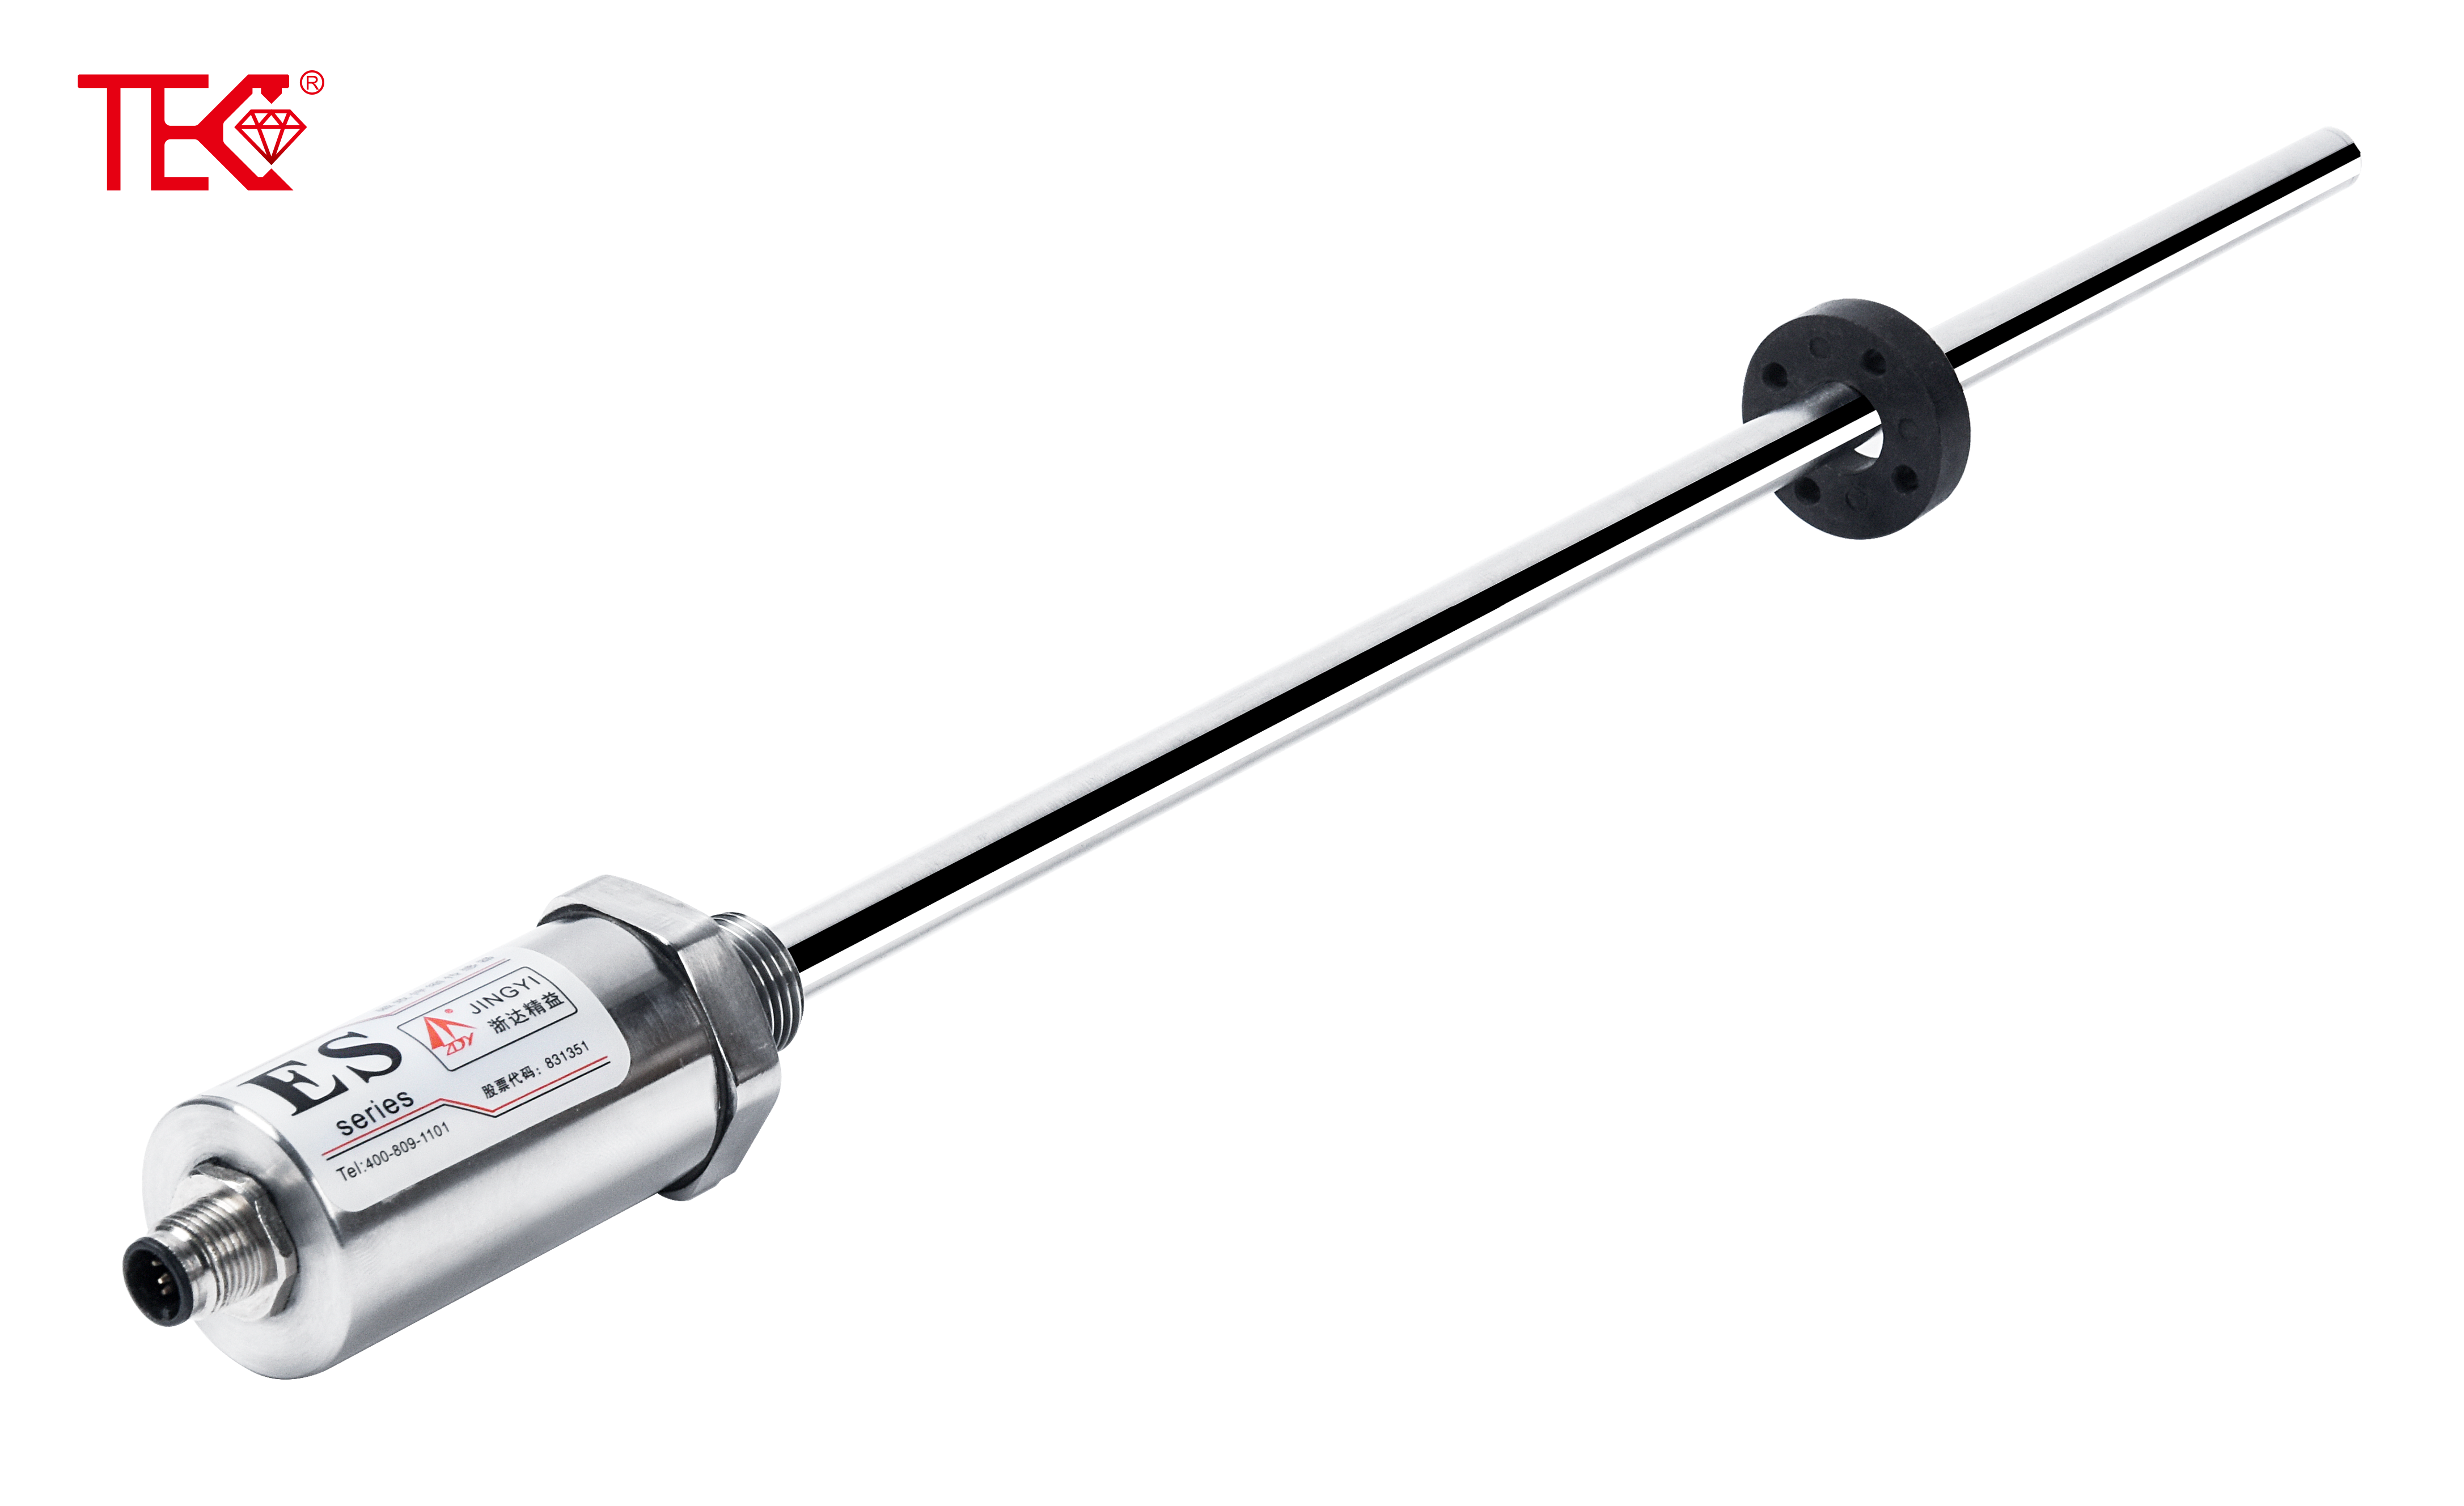
When buying an explosion-proof magnetostrictive displacement sensor for a cement bucket wheel stacker-reclaimer, price is only one part of the decision. These sensors monitor boom position, bucket wheel travel, and hydraulic cylinder movement in dusty, vibrating, and potentially explosive cement plant environments. A reliable unit must combine high linearity, long stroke options, strong EMI resistance, and certified explosion protection for continuous material handling.
Market prices usually range from about USD 300 to USD 1,500 per unit, but final cost depends on stroke length, accuracy class, output signal, housing material, cable type, and hazardous-area certification. Models with ATEX/IECEx approval, stainless steel construction, and customized connectors cost more. Brand, calibration service, lead time, warranty, and spare-part availability also affect the quotation. For large stacker-reclaimers, project-specific engineering and fast delivery may matter as much as the initial sensor price.
For cement stacker-reclaimers, choose a sensor with IP67 or higher protection, shock and vibration resistance, and stable performance under temperature changes. Confirm that the output matches the PLC or control system, such as 4-20 mA, 0-10 V, SSI, or Profibus. Ask suppliers for test reports, certificates, installation drawings, and after-sales support. Comparing total lifecycle cost is wiser than selecting the lowest initial price. A suitable sensor reduces downtime, improves positioning accuracy, and supports safe automatic operation in cement bulk material handling.
 Grain and Oil Storage Tank Rea
 Mixing Station Silo Explosion-
 Shield Tunneling Hoist High-te
 Injection Molding Die Casting