Bucket Wheel Stacker-reclaimer Explosion-proof Crane and Trolley Positioning Manufacturer
For bucket wheel stacker-reclaimers operating in coal, coke, petrochemical, and port bulk-handling yards, explosion-proof crane and trolley positioning systems are critical to safe, accurate material stacking and reclaiming. A qualified manufacturer combines flameproof electrical design, rugged mechanical engineering, and precise motion control in one integrated package. Explosion-proof cranes use certified motors, spark-free brakes, sealed control cabinets, and anti-collision protection to reduce ignition risk in hazardous dust or gas areas. Trolley positioning can be achieved with laser distance sensors, rotary encoders, absolute positioning, or redundant PLC logic, giving operators real-time feedback and reliable travel limits. The result is smoother bucket wheel movement, less cable wear, fewer misoperation events, and higher uptime. Manufacturers should provide ATEX/IECEx or regional certification support, custom travel and lifting capacities, HMI integration, commissioning, and after-sales service. Key design checks include zone classification, gas group and temperature class, dust layer ignition risk, rail alignment, wind load, braking performance, and emergency stop response. For project teams, selecting the right explosion-proof crane and trolley positioning manufacturer means matching equipment to site classification, duty cycle, and maintenance access. Factory acceptance testing, documentation, spare parts, operator training, and remote diagnostics further support long-term reliability. A well-designed system improves safety compliance, protects expensive stacker-reclaimer assets, and keeps bulk material handling operations productive.
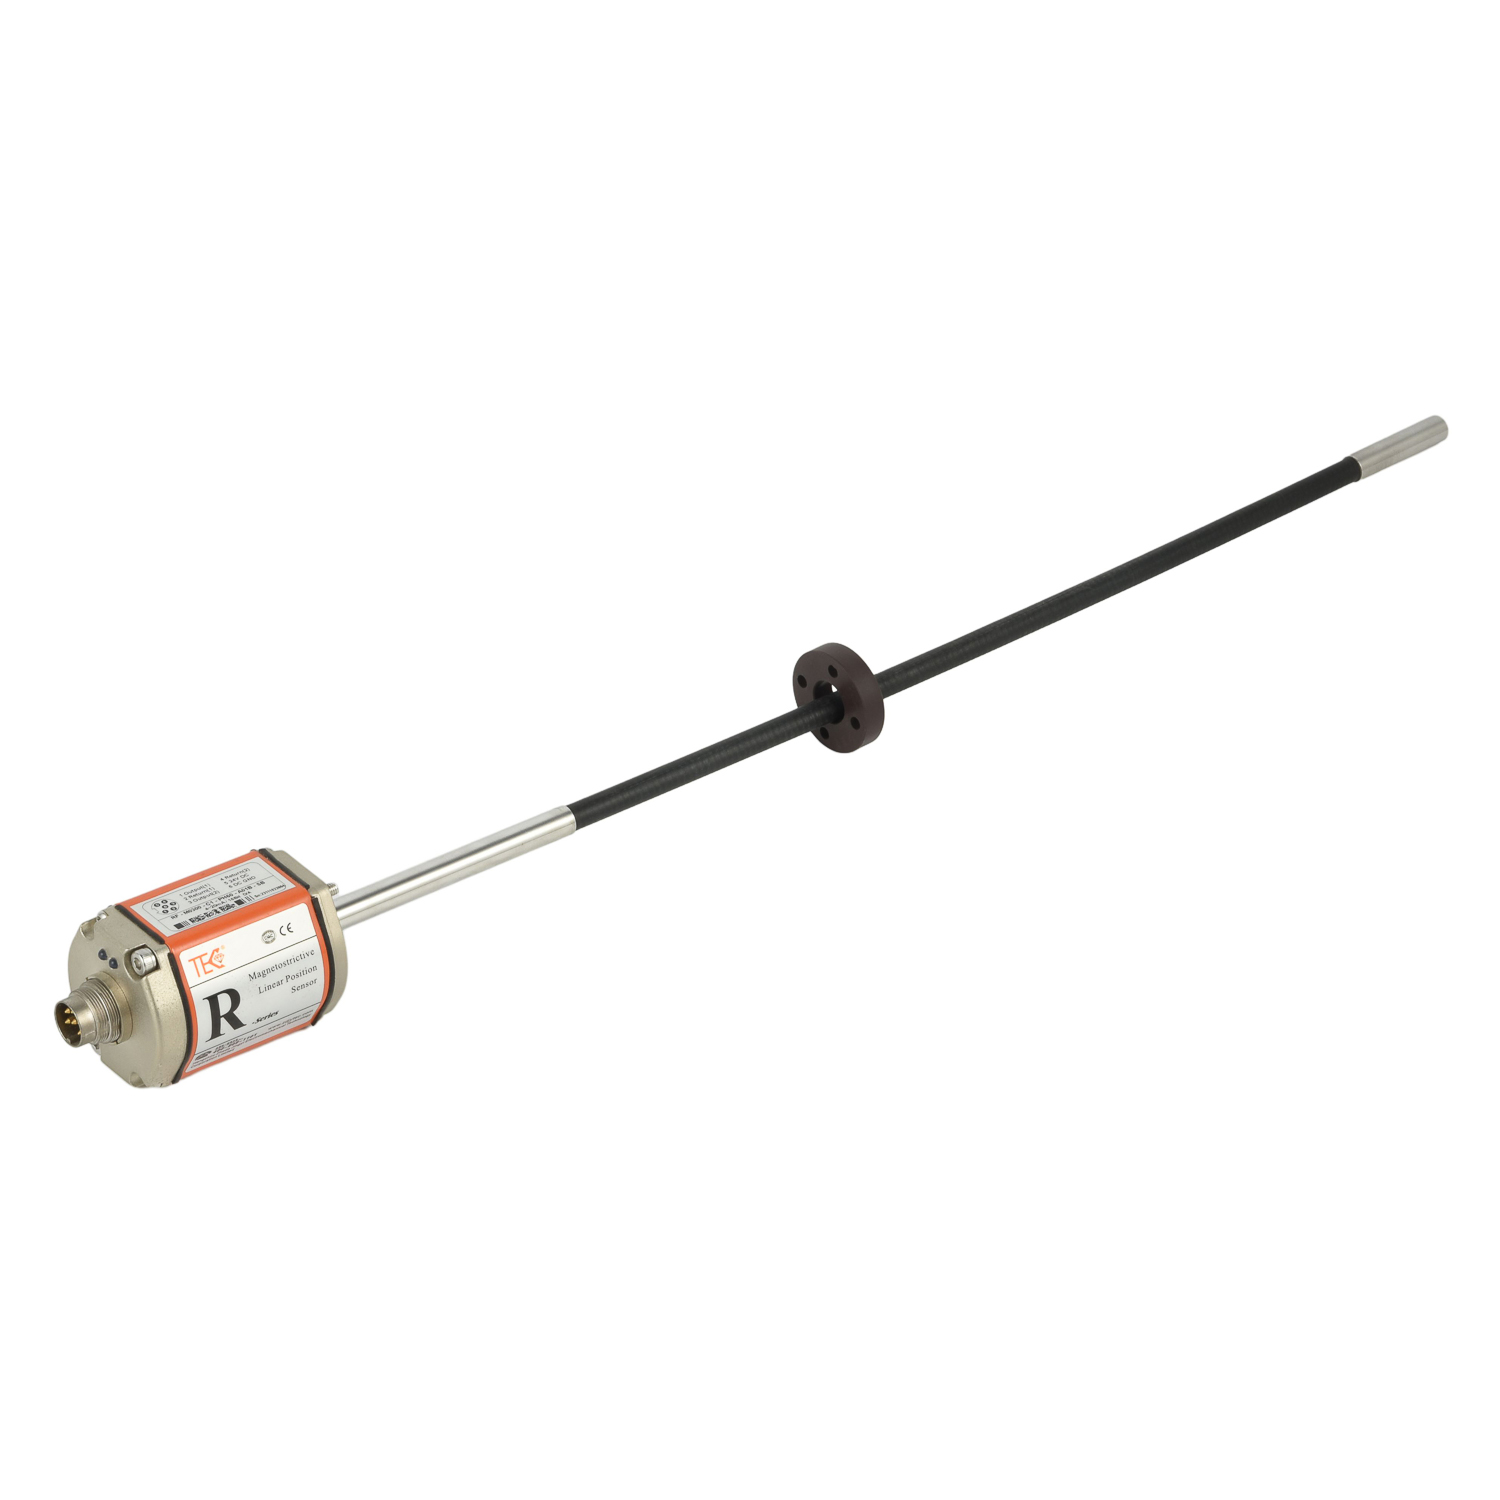
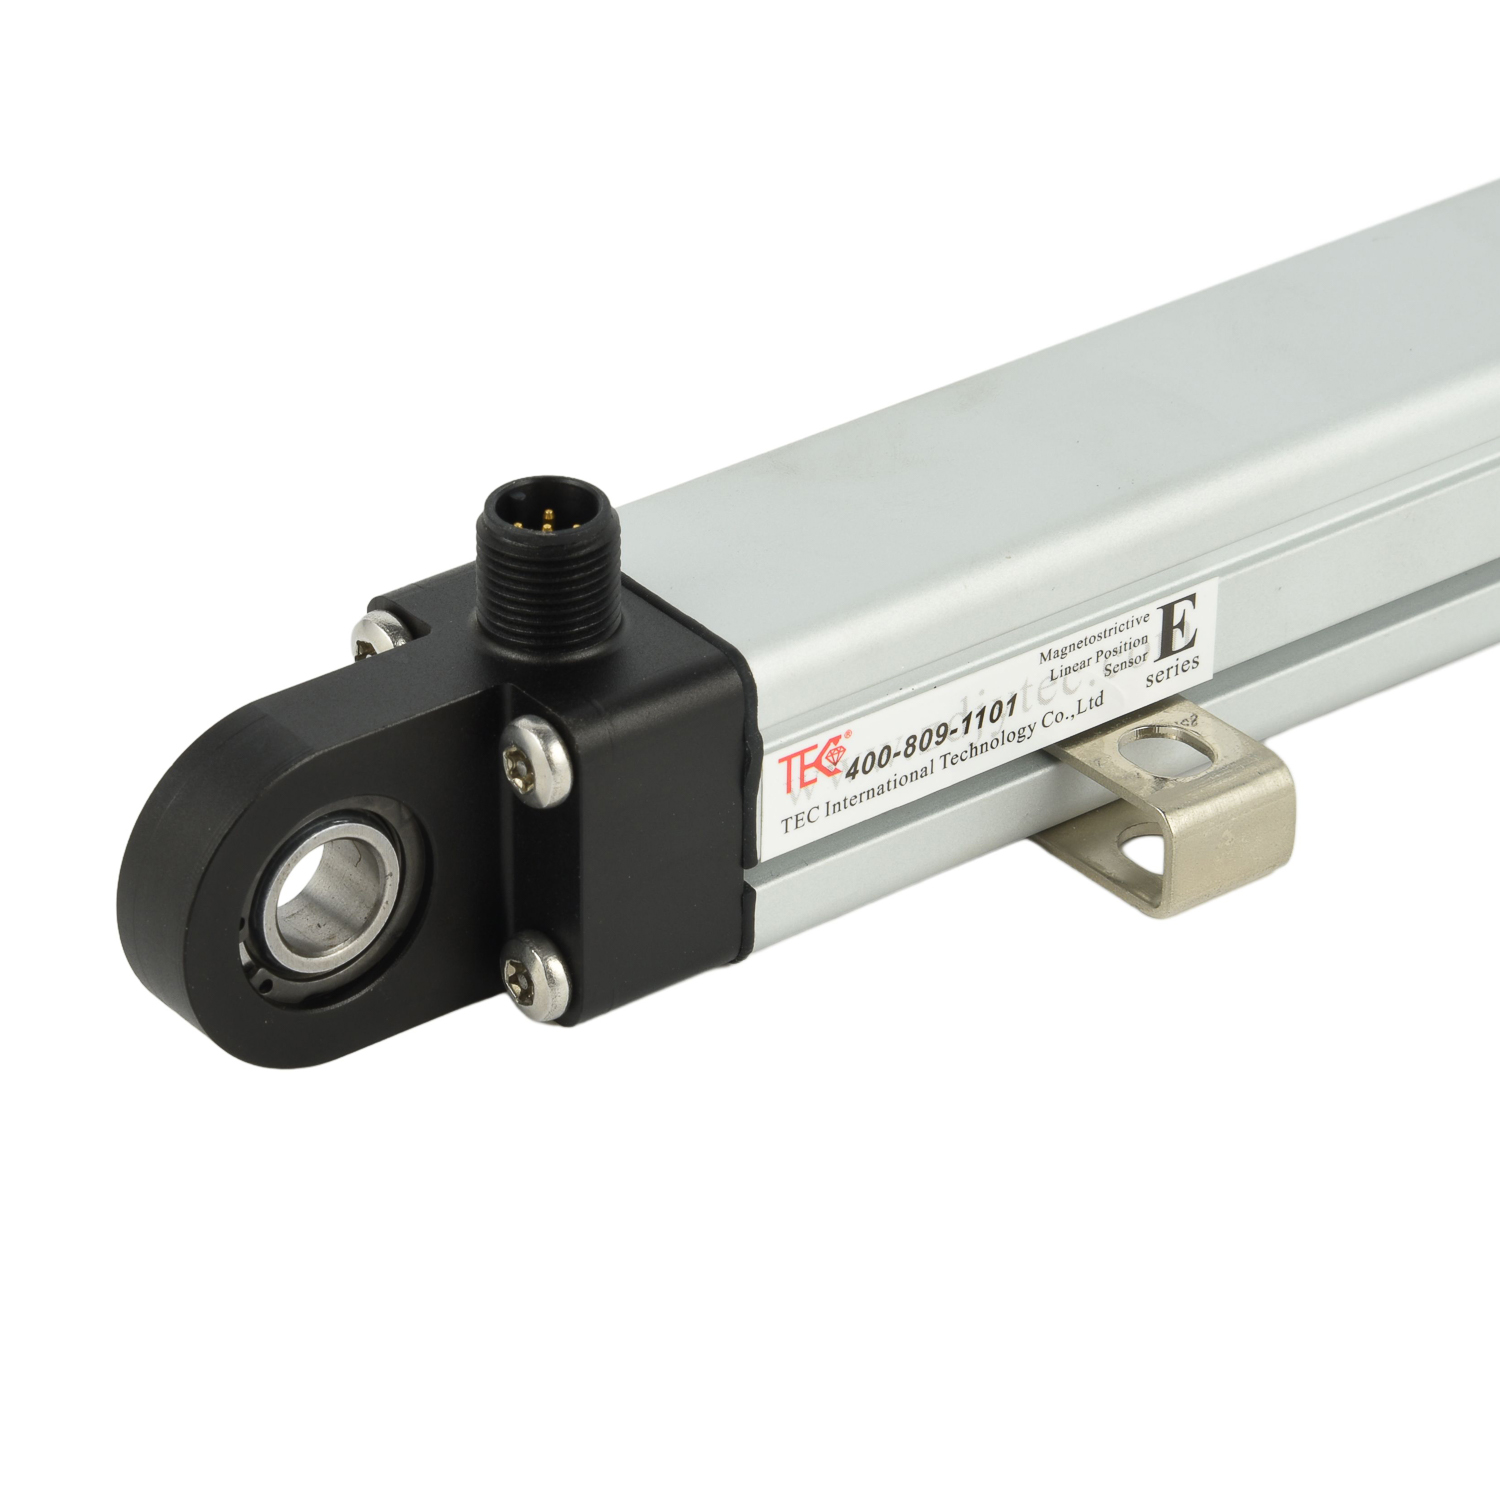 Overhead Crane High-pressure C
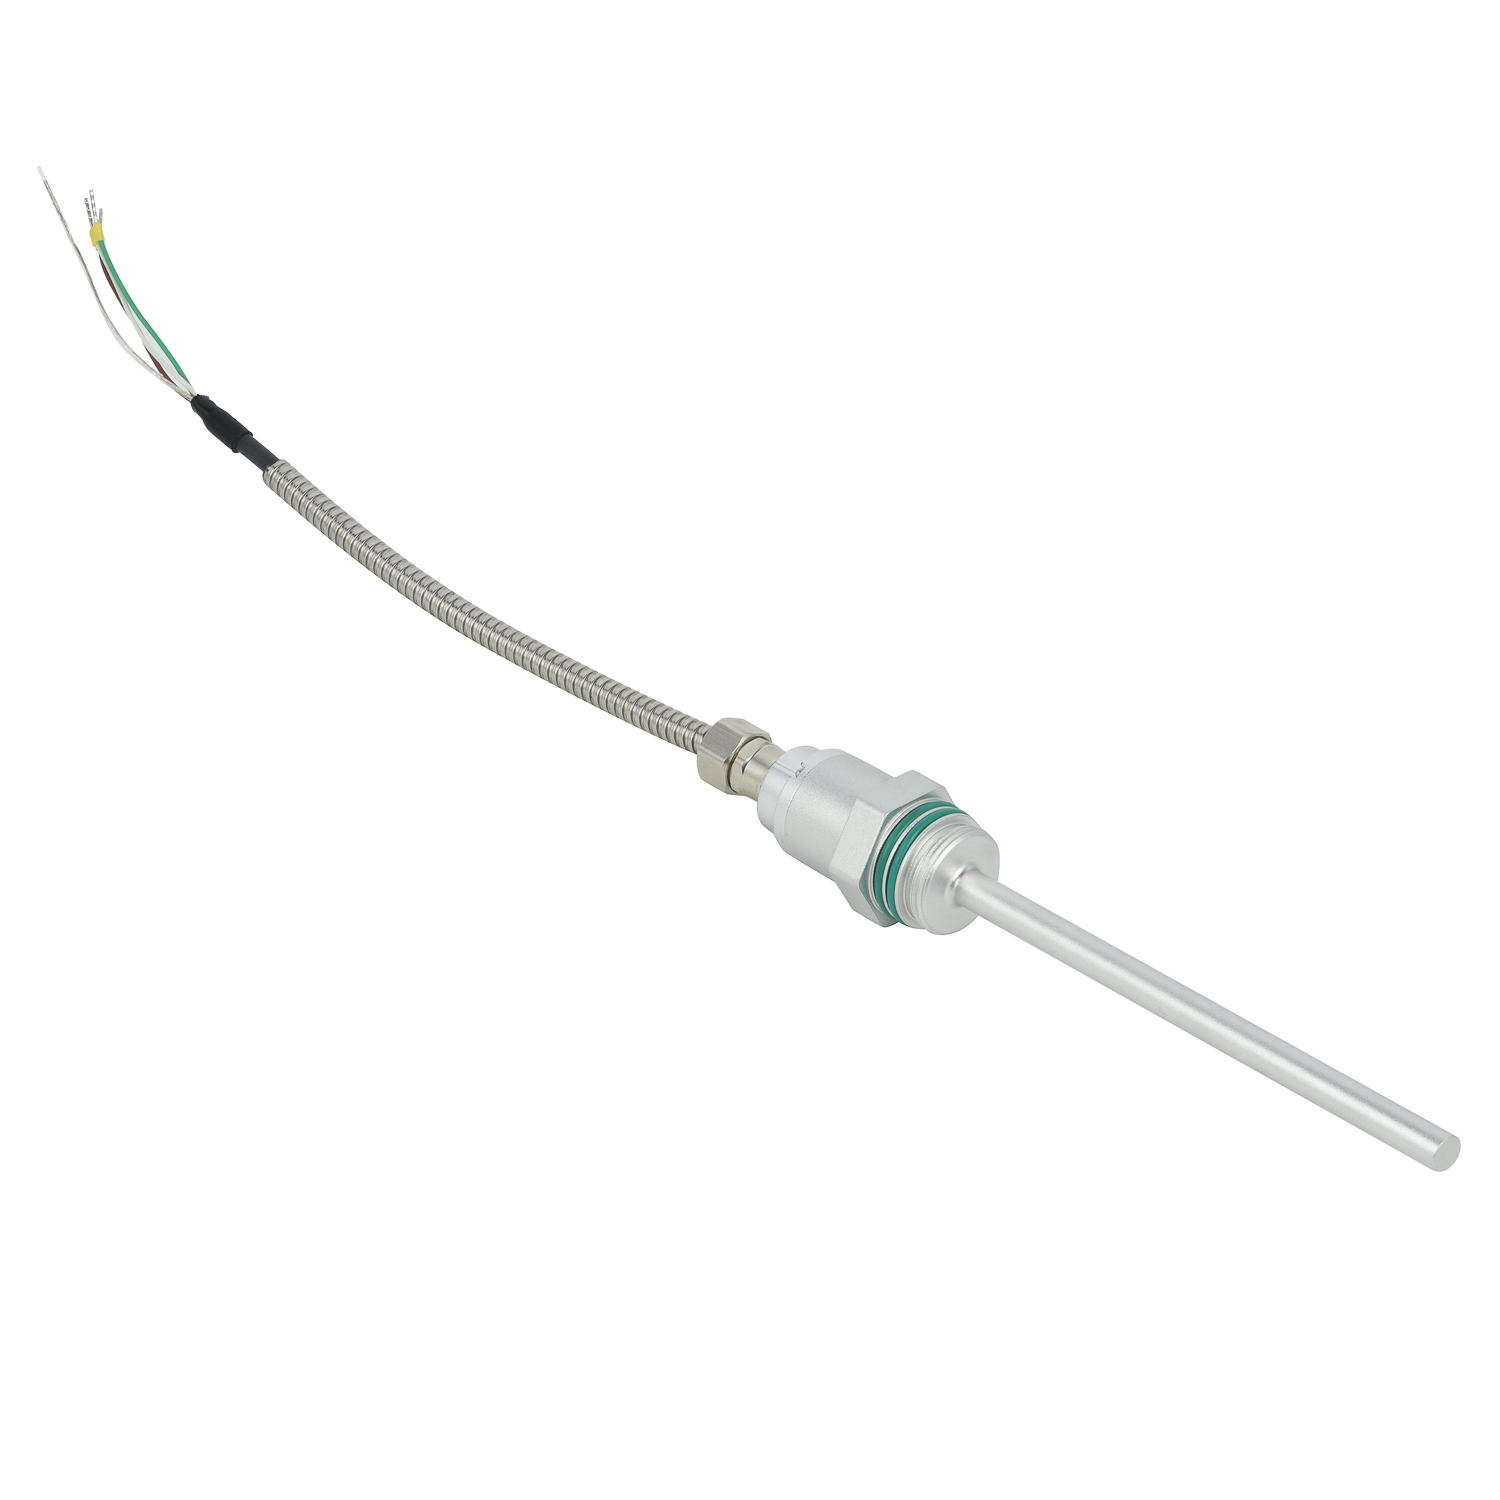 Stacker-reclaimer High-tempera
Bucket Wheel Stacker-reclaimer
 Mixing Station Explosion-proof